


Views: 0 Author: Site Editor Publish Time: 2026-08-07 Origin: Site


Thermoelectric cooler (TEC) failure often originates at the substrate level, specifically at the interface between the ceramic base and the copper metallization layer under extreme thermal cycling. Engineers must balance the need for high electrical conductivity to power the Peltier elements with the mechanical reality of Coefficient of Thermal Expansion (CTE) mismatches between copper and ceramic materials. Incorrect copper specifications lead to delamination, reduced cooling efficiency, compromised dimensional stability, or catastrophic module failure. To specify a reliable TEC ceramic substrate, procurement and engineering teams must evaluate copper bonding technologies, layer thickness, adhesion strength, dielectric characteristics, and surface finishes based on the specific thermal and electrical demands of the application. Understanding the physical behavior of metallized layers under rapid temperature shifts ensures long-term module reliability and optimal heat pumping performance in the field.
Bonding Method Dictates Application: The choice between DBC (Direct Bonded Copper), AMB (Active Metal Brazing), and DPC (Direct Plated Copper) fundamentally determines the substrate's thermal cycling lifespan, dimensional stability, and pattern resolution.
The Thickness Trade-Off: While thicker copper supports higher current, it increases mechanical stress at the ceramic interface during temperature fluctuations, requiring careful ratio balancing to prevent substrate warping.
Miniaturization Requires Plating: For a compact ceramic substrate for TEC, traditional high-temperature bonding gives way to thin-film or plated copper technologies to achieve necessary trace tolerances while maintaining dielectric isolation.
Surface Finish is Critical for Assembly: The final copper surface treatment directly impacts chemical resistance and the void-free soldering of Bismuth Telluride semiconductor pellets, which is non-negotiable for thermal transfer.
The copper layer in a Peltier module serves a dual purpose. It acts as the electrical series circuit connecting the semiconductor pellets while simultaneously functioning as the primary thermal bridge to the ceramic heat sink. If the copper layer fails in either capacity, the entire thermoelectric cooler loses efficiency or stops working entirely. Engineering teams must treat the metallization not just as a conductive path, but as a structural component of the thermal management system.
Baseline requirements for TEC metallization demand exceptional performance in two distinct areas. The copper traces must exhibit minimal electrical resistance. High resistance causes Joule heating within the traces themselves. This internal heat generation directly counteracts the cooling effect produced by the Peltier elements, drastically reducing the net cooling capacity of the module. You must specify pure, highly conductive copper to ensure the electrical current translates into cooling power rather than wasted heat.
Simultaneously, the copper must facilitate rapid thermal transfer. Heat absorbed at the cold junction must travel efficiently through the copper pads, into the ceramic base, and out to the ambient heat sink. Any thermal bottleneck in the copper layer or at the copper-ceramic interface traps heat, elevating the operating temperature of the semiconductor dies and accelerating device degradation. The thermal conductivity of the copper layer must remain consistent across the entire substrate area to prevent localized hot spots.
High-power thermoelectric modules draw significant electrical current to achieve maximum temperature differentials. The high electrical conductivity of the copper must pair perfectly with the excellent dielectric properties of the underlying ceramic. This combination prevents electrical leakage, short circuits, or arcing between adjacent traces. As modules scale up in power, the copper must carry more current without compromising the dielectric isolation provided by the ceramic base. Maintaining strict spacing and clean trace edges becomes a primary design constraint for operational safety and performance.
When designing for high voltage applications, the dielectric breakdown strength of the ceramic dictates the minimum allowable gap between copper traces. If the manufacturing process leaves copper residue or jagged edges in these gaps, the effective isolation distance decreases, increasing the risk of catastrophic electrical failure.
The physics of failure in TEC modules almost always point back to thermal mismatch. Copper possesses a relatively high Coefficient of Thermal Expansion (CTE) of approximately 16.5 ppm/K. In contrast, common ceramic materials expand and contract at much lower rates. Alumina (Al2O3) has a CTE of about 7.2 ppm/K, while Aluminum Nitride (AlN) sits even lower at roughly 4.5 ppm/K.
During the rapid hot and cold cycling inherent to TEC operation, the copper attempts to expand significantly more than the rigid ceramic base beneath it. This differential creates immense shear stress at the bonding interface. Over thousands of cycles, this stress impacts shape stability, causing the substrate to bow or warp. Severe stress ultimately leads to micro-cracking in the ceramic or complete delamination of the copper pads, instantly destroying the thermal path and breaking the electrical circuit.
Material Properties Impacting Metallization Stress
| Material | Thermal Conductivity (W/m·K) | Coefficient of Thermal Expansion (ppm/K) | Dielectric Strength (kV/mm) |
|---|---|---|---|
| Copper (Cu) | 390 - 400 | 16.5 | N/A (Conductor) |
| Alumina (Al2O3 96%) | 24 - 28 | 7.2 | > 15 |
| Aluminum Nitride (AlN) | 170 - 230 | 4.5 | > 15 |
| Silicon Nitride (Si3N4) | 80 - 90 | 3.2 | > 15 |
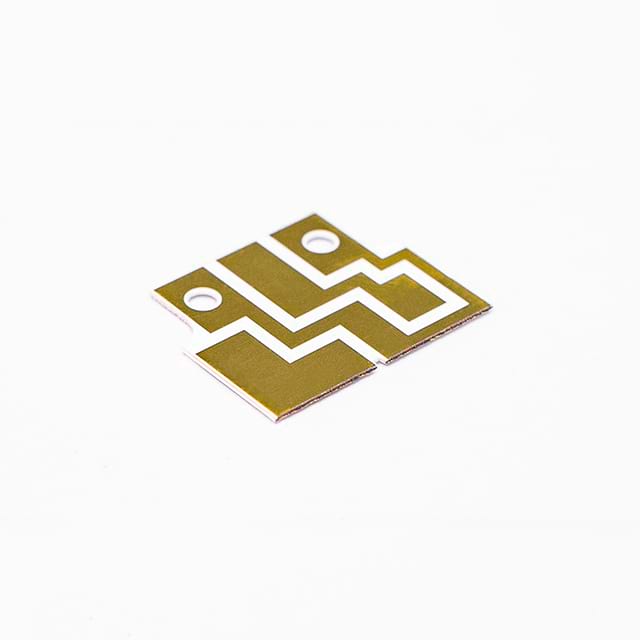
Selecting the right metallization process dictates the physical limits of your thermoelectric cooler. Industry-standard processes bond copper to ceramic in fundamentally different ways, each offering distinct advantages for specific thermal applications. You cannot apply a one-size-fits-all approach to substrate manufacturing.
Manufacturers create Direct Bonded Copper (DBC) substrates through a high-temperature oxidation process. They place thick copper foils on bare ceramic and heat the assembly in a controlled nitrogen-oxygen atmosphere to approximately 1065°C. The copper oxidizes slightly, forming a copper-oxygen eutectic melt that chemically bonds with the ceramic surface upon cooling.
DBC offers excellent thermal conductivity and exceptional current-carrying capacity. This makes it highly suitable for standard, larger-scale TECs used in industrial cooling or consumer appliances. However, DBC relies on wet chemical etching to form the circuit patterns. Etching thick copper foils results in a trapezoidal cross-section, which severely limits trace resolution and line spacing. A common engineering rule of thumb dictates that the minimum space between DBC traces must equal or exceed the thickness of the copper layer itself. You cannot achieve ultra-fine pitch layouts with standard DBC technology.
The Direct Plated Copper (DPC) process utilizes thin-film technology. Manufacturers clean the bare ceramic in a vacuum chamber and sputter a thin titanium or chromium adhesion layer, followed by a thin copper seed layer. They then use photolithography and electroplating to build up the copper thickness exactly where needed.
This additive process makes a DPC ceramic circuit board for TEC superior for high-density, low-stress applications. DPC provides vertical trace sidewalls, allowing for incredibly precise line widths and spacing. When your design requires precise alignment of micro-Peltier elements for optical or telecommunications cooling, DPC stands as the preferred route. It eliminates the heavy mechanical stress associated with thick bonded foils while delivering the exact pattern resolution required for miniaturization.
Active Metal Brazing (AMB) represents the premium solution for harsh environments. This process uses a brazing paste containing active metals like titanium, zirconium, or hafnium to chemically bond copper foil to the ceramic at high temperatures in a vacuum furnace. AMB proves especially critical when bonding copper to Aluminum Nitride (AlN) or Silicon Nitride (Si3N4), as these non-oxide ceramics lack the oxygen atoms required for standard DBC bonding.
AMB delivers maximum adhesion strength, superior dimensional stability, and unmatched thermal shock resistance. When your TEC module must survive extreme temperature gradients, rapid cycling, or high mechanical vibration, AMB ensures the copper remains firmly attached to the ceramic base without degrading over time. The active metal layer acts as a slight mechanical buffer, absorbing a portion of the shear stress generated by the CTE mismatch.
Metallization Technology Capabilities
| Process | Typical Copper Thickness | Minimum Line/Space Resolution | Adhesion Strength (Peel) |
|---|---|---|---|
| DBC | 100µm - 300µm+ | ~300µm (Depends on thickness) | > 50 N/cm |
| DPC | 10µm - 150µm | 20µm / 20µm | > 40 N/cm |
| AMB | 100µm - 800µm | ~300µm (Depends on thickness) | > 80 N/cm |
Engineering a robust module requires translating operational demands into precise manufacturing specifications. You must define specific copper attributes on your fabrication drawings to guarantee performance and reliability in the field.
Copper thickness dictates the electrical resistance and the current-carrying capacity of your substrate. Typical copper thicknesses range from 50µm for low-power micro-coolers up to 300µm or more for heavy-duty industrial modules. You must calculate the required trace width and thickness for a high current TEC ceramic substrate to prevent trace degradation.
Insufficient copper thickness leads to localized overheating, which degrades the solder joints and the semiconductor dies. However, simply maximizing copper thickness introduces severe mechanical risks. You must balance the electrical requirement for thick copper against the mechanical requirement for thermal cycling reliability. A thicker copper layer exerts exponentially more shear force on the ceramic during a temperature swing.
Steps for Calculating Trace Dimensions:
Determine the maximum continuous operating current (Imax) of the TEC module.
Establish the maximum allowable temperature rise within the copper traces (typically kept below 5°C for TECs to avoid parasitic heating).
Use standard IPC-2221 cross-sectional area formulas to find the minimum required copper area.
Divide the required area by the available trace width to determine the minimum copper thickness.
Add a 20% safety margin to account for manufacturing tolerances and localized current crowding at the trace corners.
Adhesion strength measures how forcefully the copper bonds to the ceramic. You should define acceptable peel strength metrics on your specifications, typically requiring values greater than 50 N/cm for standard applications and >80 N/cm for high-reliability environments. High initial adhesion strength provides a buffer against the shear stresses generated during operation.
Adhesion strength naturally degrades over time with continuous thermal cycling. The constant expansion and contraction fatigue the bonding interface, initiating micro-voids that eventually coalesce into full delamination. Establishing strict baseline requirements for initial peel strength ensures the substrate retains enough mechanical integrity to survive its intended operational lifespan.
Modern electronic packaging demands smaller, more efficient cooling solutions. This drives the need for tighter line width and spacing (L/S) limits. Specifying a compact ceramic substrate for TEC necessitates L/S tolerances that traditional etching cannot achieve. This requirement pushes the technology choice away from DBC toward DPC.
Even as you shrink the module, you must maintain strict spacing rules to preserve the ceramic's dielectric insulation between adjacent traces. If traces sit too close together, high voltages can cause electrical arcing across the gap. You must calculate the minimum safe distance based on the maximum operating voltage of the TEC module and the dielectric breakdown strength of the specific ceramic material. You must also account for the operating environment; high humidity or low atmospheric pressure reduces the effective breakdown voltage of the air gap between traces.
Bare copper oxidizes rapidly when exposed to air, rendering it unsolderable. You must specify a surface finish to protect the copper and ensure reliable assembly. The surface finish provides essential chemical resistance against harsh assembly fluxes and environmental oxidation. More importantly, these finishes ensure a void-free intermetallic bond when soldering the Bismuth Telluride thermoelectric dies to the substrate.
Surface Finish Selection Criteria:
Electroless Nickel Immersion Gold (ENIG): Provides a highly flat, oxidation-resistant surface ideal for the precise placement and reflow of semiconductor pellets. The nickel layer acts as a barrier preventing copper from diffusing into the solder joint.
Electroless Nickel Electroless Palladium Immersion Gold (ENEPIG): Adds a palladium layer to prevent nickel corrosion (often called "black pad" syndrome). Use this for high-reliability military or aerospace TECs.
Organic Solderability Preservatives (OSP): A low-cost, thin organic coating that protects copper until reflow. Rarely used in high-end TECs due to its limited shelf life and inability to withstand multiple thermal excursions during complex assembly processes.
Finalizing a substrate specification requires analyzing the compromises between electrical performance, mechanical reliability, and manufacturing capabilities. No single configuration excels in every category. You must prioritize the failure modes most likely to occur in your specific application.
Engineers face a well-established reliability rule: a thick and strong ceramic substrate metallized with a thin copper layer withstands significantly more thermal cycles than one with thick copper. Thin copper generates less shear force against the ceramic during temperature shifts. The ceramic easily restrains the thin copper, preventing it from expanding fully.
Conversely, thick copper on a thin ceramic base creates a severe risk of warpage. This combination acts like a bimetallic strip. As temperatures change, the dominant expansion of the thick copper forces the thinner ceramic to bow. This loss of shape stability destroys the flat thermal interface required for mounting the TEC to a heat sink. A bowed substrate creates air gaps between the TEC and the heat sink, which act as massive thermal insulators. You must utilize a decision framework that balances the need for high current against the need for longevity and flatness.
Recommended Copper-to-Ceramic Thickness Ratios
| Ceramic Base Thickness | Maximum Recommended Copper Thickness (DBC) | Warpage Risk Level |
|---|---|---|
| 0.38 mm | 0.15 mm | High |
| 0.63 mm | 0.30 mm | Medium |
| 1.00 mm | 0.40 mm | Low |
The choice of base ceramic fundamentally alters your copper specification strategy. Aluminum Nitride (AlN) offers exceptional thermal conductivity, making it highly desirable for high-power TECs. However, AlN presents higher CTE mismatch risks with thick copper compared to Alumina (Al2O3).
Because AlN expands very little, the differential between the copper and the AlN is massive. Bonding thick copper to AlN using standard DBC processes often results in immediate ceramic cracking during the cool-down phase of manufacturing. The copper contracts violently, tearing the rigid AlN apart. To utilize thick copper on AlN safely, you must specify AMB technology. The active metal brazing layer absorbs some of the mechanical stress, preventing the ceramic from fracturing.
Even with perfect specifications, manufacturing realities introduce risks. Understanding common failures related to the copper layer allows you to implement robust prevention strategies before mass production begins.
During the bonding process, micro-voids or gas bubbles can become trapped between the copper and the ceramic. These voids act as microscopic thermal insulators. When a TEC operates, heat cannot pass through these voids, creating localized hot spots that degrade the semiconductor dies directly above them. Over time, these hot spots cause the solder joints to melt or the semiconductor material to fracture.
To mitigate this risk, you must specify Scanning Acoustic Microscopy (SAM) testing in your supplier Quality Assurance (QA) requirements. SAM uses high-frequency sound waves to non-destructively detect internal voids. Establish a strict acceptance criterion, such as rejecting any substrate with individual voids larger than 1% of the total pad area or a total void area exceeding 5%.
The edges of the copper pads experience the highest concentration of shear stress during rapid temperature shifts. This stress causes the copper to peel away from the ceramic, starting at the corners and propagating inward. Once delamination begins, it accelerates rapidly because the reduced contact area forces the remaining bond to handle even more stress.
You can mitigate this delamination risk by implementing specific design rules on your copper layout. Use dimpling (creating small unplated holes in large copper areas) to break up continuous stress fields. Implement edge step-backs, ensuring the copper does not extend all the way to the physical edge of the ceramic. You can also specify stress-relief etching, which rounds the corners of the copper pads to eliminate sharp stress concentration points.
Ensure your manufacturing partner executes mandatory reliability tests before approving a production batch. You cannot rely solely on visual inspections to verify substrate integrity.
Mandatory QA Testing Protocols:
Thermal Shock Testing: Cycle the substrates from -40°C to +150°C for a minimum of 500 cycles (liquid-to-liquid transfer provides the most rigorous test).
High-Temperature Storage: Bake the substrates at 150°C for 1000 hours to verify the stability of the surface finish and check for intermetallic compound degradation.
Post-Cycling Shear Strength: Perform destructive shear testing on the copper pads after thermal cycling to confirm the adhesion has not degraded below your specified minimum threshold.
Dielectric Withstanding Voltage: Apply high voltage across adjacent traces to ensure no micro-cracking has compromised the ceramic's isolation properties.
The optimal copper features for a TEC ceramic substrate represent a calculated compromise between electrical current demands, thermal cycling severity, dielectric requirements, and overall module size. Understanding the physics of thermal mismatch and the capabilities of different metallization processes ensures you specify a substrate that survives its intended environment without failing prematurely.
Use clear shortlisting logic for your next project. For high-current, standard-size industrial cooling, specify DBC with balanced copper-to-ceramic thickness ratios to maintain shape stability. For micro-cooling and optical applications, specify DPC to achieve necessary trace precision and miniaturization. For extreme reliability and high-power density, specify AMB on AlN.
Take the following actionable steps before finalizing your design:
Run comprehensive thermal and mechanical simulations on CTE mismatch prior to prototyping.
Request historical thermal cycling reliability data, including SAM imagery post-1000 cycles, from potential substrate manufacturers.
Define your surface finish requirements based strictly on the specific solder paste and flux chemistry used in your die-attach assembly process.
Implement edge step-backs and stress-relief dimpling in your CAD layout for all large copper pads.
A: The ideal thickness typically ranges from 150µm to 300µm to handle high electrical loads without excessive Joule heating. However, you must balance this thick copper with a proportionally thicker ceramic base layer. Failing to maintain this ratio leads to severe bowing, loss of dimensional stability, or complete delamination under thermal stress.
A: DPC uses a thin-film sputtering and electroplating process rather than etching thick foils. This additive method allows for extremely fine line and space resolution, often down to 10-20µm. Such precision is impossible to achieve with standard etched DBC, making DPC the only viable choice for a highly compact ceramic substrate for TEC.
A: Repeated heating and cooling creates intense shear stress at the copper-ceramic interface due to CTE mismatch. High initial adhesion strength ensures the copper traces do not lift, peel, or break the electrical circuit over time. Strong adhesion directly correlates to the thermal cycling lifespan of the module.
A: Yes, but it carries significant risk. AlN has a much lower CTE than Alumina, making the mechanical mismatch with copper far more severe. Bonding thick copper to AlN typically requires Active Metal Brazing (AMB) technology. Standard DBC processes often cause the AlN ceramic to crack during manufacturing or early thermal cycling.
A: ENIG (Electroless Nickel Immersion Gold) or ENEPIG are highly recommended. These finishes provide excellent chemical resistance against aggressive fluxes. More importantly, they create a perfectly flat, oxidation-free surface that promotes strong, void-free solder joints, which are absolutely essential for efficient thermal transfer from the die to the copper.


