


Views: 0 Author: Site Editor Publish Time: 2026-08-28 Origin: Site


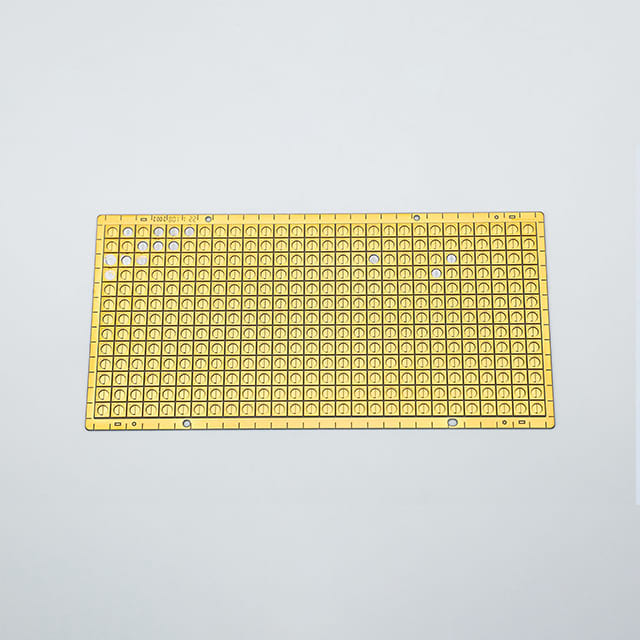
High-power LEDs fail primarily due to inadequate thermal management, where microscopic thermal bottlenecks lead to critical junction temperature spikes. Excessive junction heat directly causes wavelength shift, accelerated phosphor degradation, and drastically reduced luminous efficiency, compromising product viability in demanding environments. Transitioning from traditional Metal Core PCBs (MCPCBs) to engineered ceramic solutions is a necessary architectural shift for manufacturers requiring high-density packaging, sustained brightness, and verifiable long-term reliability. We see this failure mode constantly in the field. You push the drive current, the die heats up, and the organic dielectric layer in a standard board chokes the heat transfer. The result is a dead array. Moving to ceramics removes that bottleneck entirely, providing a direct, high-efficiency thermal pathway from the semiconductor die straight to the external heatsink.
Integrating an optimized ceramic substrate can reduce overall thermal resistance by 50–70% compared to standard FR4 or traditional metal-core alternatives.
Maintaining LED junction temperatures strictly below 120°C is the baseline requirement for achieving and certifying 25,000+ hour operational lifespans.
Beyond raw heat dissipation, ceramic substrates drastically improve temperature uniformity across the array, preventing localized hot spots that cause uneven color rendering.
Material selection—ranging from high-purity Alumina to Aluminum Nitride—dictates the precise balance between thermal conductivity, mechanical fracture toughness, and unit cost.
Advanced metallization techniques, specifically Direct Plated Copper (DPC), provide the necessary thermal pathways and fine-pitch resolution required for modern micro-LED and automotive arrays.
Junction temperature represents the absolute highest operating temperature generated within the actual semiconductor diode during active operation. When electrical energy converts into visible light, inherent physical inefficiencies generate residual thermal energy. If this heat cannot escape the package structure, the junction temperature rises rapidly. Elevated temperatures exponentially increase non-radiative recombination rates within the semiconductor lattice. This physical reaction directly degrades lumen output and accelerates the physical breakdown of the surrounding phosphor matrix. We measure this degradation in real-time during accelerated life testing, and the data always points back to trapped heat at the junction.
Heat dissipation follows a strict, sequential thermal pathway. You must map this route to understand where the system fails. Thermal energy moves from the semiconductor die through the die attach material. It then travels across the substrate structure before finally reaching the external heatsink. Thermal resistance accumulates at every single physical interface along this route. Legacy packaging architectures rely on substrates that inherently act as severe thermal bottlenecks. Standard FR4 composite boards or basic metal-core designs restrict rapid heat transfer due to their material limitations.
The primary success criterion for modern packaging involves maximizing thermal conductivity while maintaining absolute electrical isolation. Temperature uniformity across the entire substrate surface is equally critical. Multi-die packages suffer severe performance degradation when localized thermal runaway occurs. Isolated hot spots cause uneven color rendering across the spectrum and accelerate cascading die failures. A high-performance substrate must spread heat laterally with extreme efficiency. This lateral dispersion ensures consistent light output across the entire diode array and protects adjacent components from thermal spillover.
Standard Thermal Pathway Interfaces
Semiconductor Die (Heat Generation Source)
Die Attach Solder or Silver Epoxy
Substrate Top Metallization Layer
Substrate Core Material
Substrate Bottom Metallization Layer
Thermal Interface Material (TIM)
External Aluminum or Copper Heatsink
Traditional Metal Core PCBs contain a fundamental structural flaw engineered directly into their design. They rely entirely on thermally resistive epoxy-based dielectric layers to separate the copper circuitry from the aluminum base. These organic layers typically yield a maximum thermal conductivity of only 1 to 3 W/m·K. This creates a massive, unavoidable barrier to vertical heat dissipation. Furthermore, organic dielectrics degrade over time when exposed to continuous high-temperature cycling, leading to eventual dielectric breakdown and catastrophic electrical shorts. We pull failed MCPCBs from the field regularly, and the failure point is almost always a scorched dielectric layer.
Integrating an LED ceramic substrate offers a distinct dual-nature advantage. Inorganic ceramics act simultaneously as high-voltage electrical insulators and highly efficient thermal conductors. This unique material architecture entirely eliminates the need for a vulnerable organic thermal interface material layer. Heat transfers directly from the metallization layer into the ceramic core without encountering an insulating epoxy barrier. You get a straight shot from the heat source to the dissipation zone.
This direct-heat-draw architecture represents a proven standard across multiple high-stress engineering disciplines. It dominates mission-critical power semiconductor modules where overheating leads to immediate system failure. Removing the dielectric bottleneck allows thermal energy to flow unimpeded from the die to the heatsink. This structural advantage prevents the thermal pump-out effect commonly observed in standard organic interface materials.
Aggressive thermal cycling induces severe mechanical stress on all electronic assemblies. As components heat up and cool down, they expand and contract at different rates. Ceramic materials possess a Coefficient of Thermal Expansion ranging from 4.5 to 7.5 ppm/°C. This specific expansion rate closely matches common high-power LED semiconductor chips, including Gallium Nitride and Silicon Carbide. When the chip and the board expand at the same rate, the mechanical stress on the connection points drops to near zero.
Standard aluminum or copper boards expand rapidly when heated, exhibiting CTE values often exceeding 20 ppm/°C. This severe mismatch causes intense shear stress at the physical connection points between the die and the board. Closely matched CTE in ceramic solutions prevents solder joint fatigue. It eliminates microscopic crack propagation and stops layer delamination during rigorous thermal cycling. Reliable, intact solder joints ensure uninterrupted electrical delivery and maintain the critical thermal pathways over the entire product lifespan.
Substrate Material Performance Comparison
| Substrate Type | Dielectric Thermal Conductivity | CTE (ppm/°C) | Failure Mode Under High Load |
|---|---|---|---|
| Standard FR4 | 0.3 - 0.4 W/m·K | 14 - 17 | Rapid carbonization, delamination |
| Aluminum MCPCB | 1.0 - 3.0 W/m·K | 22 - 24 | Dielectric breakdown, solder shear |
| Alumina Ceramic | 24 - 30 W/m·K | 6.5 - 7.5 | Mechanical fracture if mishandled |
| Aluminum Nitride | 170 - 230 W/m·K | 4.5 - 5.5 | Hydrolysis if improperly sealed |

High-purity alumina, typically ranging from 96% to 99% purity, serves as the reliable performance baseline for the majority of lighting applications. It offers highly stable dielectric properties across a wide operational spectrum. Electrical conductivity changes remain strictly minimal even at extreme ambient temperatures exceeding 400°C. Alumina provides moderate thermal conductivity, generally measuring between 20 and 30 W/m·K, which adequately handles standard heat loads. We specify this material for the vast majority of general illumination projects because it works predictably.
Standard commercial high-power lighting fixtures rely heavily on alumina substrates. Industrial applications also benefit from its balanced mechanical properties and accessible manufacturing processes. However, alumina presents specific engineering trade-offs. It lacks sufficient thermal dissipation capabilities for ultra-high-density diode arrays. Deep-UV LEDs also generate concentrated heat loads that quickly exceed alumina's maximum thermal transfer limits, necessitating alternative materials.
Aluminum nitride delivers exceptional thermal conductivity designed for extreme environments. Performance ranges from 170 to 230 W/m·K depending on the specific manufacturing process and grain boundary optimization. This thermal efficiency closely approaches that of beryllium oxide but entirely avoids the severe toxicity risks associated with beryllium dust exposure during manufacturing. When you have a massive thermal load packed into a tiny footprint, AlN is the only viable option.
Dense LED arrays require rapid, aggressive heat spreading to survive continuous operation. Laser diodes and high-power UV LEDs also demand immediate thermal extraction to maintain specific wavelength outputs. Aluminum nitride excels in these demanding, high-wattage environments. The primary trade-offs include higher raw material processing requirements. Additionally, AlN shows potential susceptibility to hydrolysis if exposed to high moisture levels. Manufacturing, assembly, and storage protocols require strict environmental controls to prevent material degradation before final hermetic sealing.
Silicon nitride stands out primarily for its superior mechanical strength and physical durability. It boasts exceptionally high fracture toughness compared to all other technical ceramics. Thermal conductivity remains moderate to high, reaching up to 90 W/m·K, providing an excellent balance between physical resilience and heat management. You can drop a silicon nitride board, subject it to heavy vibration, or hit it with rapid thermal shock, and it will hold together.
Engineers specify silicon nitride strictly for harsh physical environments. Applications subjected to extreme mechanical stress require this specific durability. Heavy industrial vibration, constant mechanical shock, and rapid thermal cycling will easily shatter weaker materials like standard alumina. Silicon nitride maintains absolute structural integrity while providing more than adequate thermal dissipation for high-power components.
Direct Plated Copper technology utilizes advanced vacuum sputtering to deposit a microscopic titanium adhesion layer directly onto the ceramic surface. This is immediately followed by precision copper electroplating. This specific manufacturing process ensures high alignment accuracy and excellent surface flatness across the entire board. We use this process when the routing tolerances leave zero room for error.
A DPC ceramic board for LED lighting allows for ultra-fine line resolution previously impossible with older technologies. It supports precise via filling and vertical interconnects. These microscopic features are critical for reducing thermal resistance in modern designs. Compact, high-density packages rely entirely on DPC to maintain tight diode spacing without compromising the necessary heat transfer pathways. You can etch the copper down to incredibly fine pitches, allowing you to pack more dies into a smaller area.
Applications requiring massive current-carrying capacity demand significantly thicker copper layers. Direct Bond Copper and Active Metal Brazing fulfill this specific electrical requirement. DBC bonds thick copper foil to the ceramic using a high-temperature eutectic melt process. AMB uses an active metal filler paste to braze the copper, offering superior adhesion strength on difficult materials like Aluminum Nitride and Silicon Nitride. We deploy these when the amperage would simply melt thinner plated traces.
A clear engineering trade-off exists between these metallization technologies. DBC and AMB provide unmatched current handling capabilities for heavy industrial applications. However, they completely sacrifice the fine-line resolution achievable with DPC. Thick copper layers cannot be chemically etched with the same microscopic precision as plated copper, limiting their use in miniaturized arrays. You have to choose between current capacity and routing density.
Complex electrical routing requirements necessitate double-layer packaging substrates. These advanced designs allow engineers to separate heavy power delivery lines from sensitive digital signal traces effectively. This separation prevents electromagnetic interference while maintaining optimal thermal pathways. We stack the layers carefully to ensure the heat still has a direct route to the bottom of the package.
Multi-layer structures support blind and buried vias within the ceramic core. They enable high-density interconnects without obstructing the primary downward thermal flow. This sophisticated routing enables advanced matrix designs. Smart adaptive lighting systems, pixelated headlight arrays, and dynamic beam technologies rely heavily on multi-layer architectures to function reliably.
Automotive lighting systems must meet stringent AEC-Q101 reliability standards before deployment. They operate continuously in exceptionally harsh environments. High ambient under-hood heat, extreme winter temperatures, and constant road vibration degrade standard electronic components rapidly. We run these boards through hundreds of thermal shock cycles from -55°C to +150°C just to validate the baseline design.
An automotive LED ceramic substrate provides the necessary physical durability to survive these conditions. CTE-matched, high-reliability substrates prevent catastrophic headlight failure during extreme weather fluctuations. They ensure precise beam patterns remain optically stable over time. Eliminating thermal distortion prevents dangerous color shifting and maintains legal road illumination standards over the entire lifespan of the vehicle.
Mini and Micro display matrices face extreme engineering demands regarding absolute miniaturization. Thousands of microscopic diodes must pack into incredibly tight configurations to achieve high-resolution visual output. Heat density in these applications reaches critical levels almost instantly upon activation. You cannot use standard routing techniques here; the physical space simply does not exist.
A micro ceramic circuit board for LED meets the strict requirement for ultra-fine pitch metallization. Superior dimensional stability prevents board warping during the high-heat reflow assembly process. Flawless surface planarity ensures uniform light emission across the entire display matrix. Even microscopic surface deviations will cause dead pixels, uneven brightness, or visible dark spots on high-resolution commercial displays.
Ceramic materials possess inherent physical brittleness. This specific physical characteristic leads to potential yield loss during panel singulation, robotic handling, and final assembly. Mechanical stress applied during mounting easily induces microscopic fractures that compromise both electrical isolation and thermal conductivity. If a technician torques a mounting screw too hard, the board will crack instantly.
Mitigation requires implementing strict, specialized process controls. Specify optimized laser depaneling parameters to ensure clean cuts without micro-cracking. Implement automated vacuum handling protocols on the assembly line to eliminate manual bending stress. Design specific stress-relief features directly into the board layout to isolate sensitive diode areas from mechanical mounting pressure caused by screws or clamps.
Evaluating financial viability requires looking beyond the initial unit purchase price. Weigh the higher initial manufacturing cost of ceramic substrates against the verifiable long-term operational benefits. Standard FR4 boards appear cheaper initially but fail rapidly under high thermal loads. We see companies try to save money on the substrate, only to lose thousands in field replacements and damaged reputations.
Ceramics enable extended operational lifespans easily exceeding 25,000 hours. They drastically reduce warranty claims related to premature thermal failure and color degradation. Highly efficient substrates often allow engineers to completely eliminate secondary cooling components like bulky aluminum heatsinks or active cooling fans. Justify the premium of Aluminum Nitride or DPC boards strictly in mission-critical or thermally extreme applications where standard organic materials guarantee rapid system failure.
Run thermal simulations in Ansys or Flotherm to map heat distribution across your proposed substrate material accurately.
Order DPC ceramic prototype samples to validate fine-pitch routing and automated assembly compatibility on your production line.
Execute accelerated life testing (ALT) on the assembled modules to verify junction temperature reductions under maximum drive current.
Redesign mechanical mounting fixtures to include stress-relief cutouts, preventing micro-fractures during final hardware installation.
A: Ceramic substrates effectively manage heat to keep junction temperatures strictly below the critical 120°C threshold. While the ceramic material itself withstands temperatures exceeding 400°C without degrading, the primary goal remains rapidly pulling heat away from the semiconductor die to prevent luminous depreciation and phosphor degradation.
A: DPC provides ultra-fine line resolution and exact via filling, optimizing thermal pathways for compact, high-density arrays. DBC uses thicker copper layers, which handles higher electrical currents better but sacrifices the microscopic routing precision required for miniaturized matrices.
A: Coefficient of Thermal Expansion matching ensures the substrate expands and contracts at the exact same rate as the semiconductor chip. This prevents severe mechanical shear stress on the solder joints, eliminating micro-cracking, delamination, and premature electrical failure during rapid thermal cycling.
A: Aluminum nitride offers exceptional thermal conductivity but remains susceptible to hydrolysis when exposed to high moisture levels. Using AlN in high-humidity environments requires strict manufacturing controls, proper surface passivation, and hermetic sealing within the final package to prevent material degradation.
A: Silicon Nitride serves as the premier alternative for extreme mechanical stress. It offers significantly higher fracture toughness and superior mechanical strength compared to standard alumina, making it ideal for automotive or industrial applications subjected to heavy vibration and rapid thermal shock.
A: Multi-layer ceramic structures allow for complex electrical routing, blind vias, and high-density interconnects without obstructing the primary downward thermal pathway. When engineered correctly, they maintain extremely low thermal resistance while enabling sophisticated, densely packed matrix designs.


